Review Analysis Conclusion
Based on analysis of 9,459 reviews across the top ten welding gas regulators, a few clear patterns stand out for shoppers trying to pick the right unit. The strongest-scoring models all share three traits buyers mention again and again: stable flowmeter behavior after months of use, leak-free fittings at the cylinder neck, and gauges that stay readable instead of fogging up in humid shops. Units in the 10–60 CFH range collect the most consistent praise because they cover both light TIG work and heavier MIG passes without forcing welders to push the ball to the top of the tube.
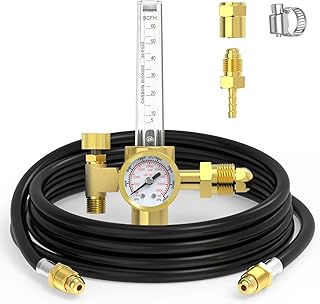
Regulators that include a hose in the box tend to earn slightly higher satisfaction scores, mostly because buyers avoid the guesswork of matching a hose end to their specific torch. Models sold without a hose still perform well in feedback, but reviewers more often mention compatibility concerns or the need for an extra adapter. Review volume also matters: the highest-ranked options each carry thousands of reviews, which gives a much clearer signal about long-term reliability than units with only a few hundred ratings.
For most welders, the takeaway from the review data is straightforward. Pick a CGA580 flowmeter whose range matches your dominant process, prioritize leak-proof construction over extra ports you will never use, and choose a hose length that fits your shop layout. Following those three signals from the strongest-reviewed models leads to a regulator that holds calibration, protects your shielding gas, and quietly does its job for years.
Buying Guide
A welding gas regulator does more than drop cylinder pressure to a usable level. It controls the flow of shielding gas that protects your molten puddle from atmospheric contamination. Picking the right unit for your MIG or TIG setup will improve bead quality, reduce porosity, and save money by preventing gas waste. This guide breaks down what actually matters when comparing the best welding gas regulators, from flow range to fitting style to long-term reliability.
Key Specs to Compare
Before looking at brand names, line up the specifications that change how a regulator performs on the job.
- Inlet connection: CGA580 is the North American standard for argon, helium, and mixed shielding gases. CO2 and argon/CO2 mixes for MIG also use CGA580 on most cylinders.
- Inlet pressure rating: Look for a gauge that reads at least 0–4000 PSI so you can clearly see remaining cylinder pressure before tank drop-off.
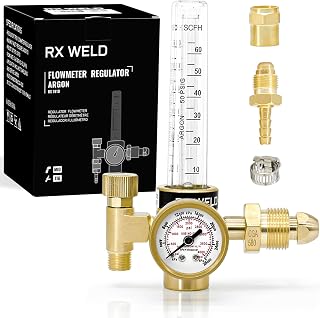
- Flow range: Match the range to your dominant process. 0–30 CFH suits thin-sheet TIG, 0–40 CFH gives finer low-end control, and 10–60 CFH covers the widest mix of MIG and TIG work.
- Outlet fittings: 9/16-inch and 5/8-inch threads plus a 1/4-inch barb cover most modern MIG and TIG torches without adapters.
- Body material: Brass and brass-alloy bodies resist corrosion and handle thermal cycling better than plated steel.
- Hose length: 6.6-foot hoses suit compact carts, while 8.2-foot hoses let you park the cylinder farther from the weld table.
Best For
- MIG welders running solid wire on mild steel: A flowmeter regulator in the 20–60 CFH range with a CGA580 inlet and dual outlets.
- TIG welders on aluminum or thin stainless: A 0–40 CFH regulator with a precise ball-type flowmeter so you can dial in low, steady shielding flow.
- Hobbyists with one welder and a small bottle: A compact dual-gauge model with a 0–30+ CFH range that fits tight cart setups.
- Shops that switch between argon, helium, and CO2: A multi-gas compatible flowmeter rated for all three shielding gases.
- Production or long-weld environments: A dual-stage regulator that keeps outlet pressure stable as the cylinder drains.
Avoid If
- You only run short TIG beads on thin material: A 10–60 CFH flowmeter can feel coarse at the low end. A 0–30 or 0–40 CFH model gives more precise low-flow control.
- Your cylinder valve is not CGA580: Some older or specialty tanks use different inlets. Confirm the connection before buying.
- You need to mount the regulator in a very tight space: Flowmeter tubes and dual gauges add height and width. Measure clearance above the cylinder valve first.
- You rely on helium-rich mixes for heavy aluminum: A basic argon/CO2 regulator will not give you the flow capacity you need. Look for a model rated for helium.
Common Mistakes
- Cracking the cylinder valve while standing in front of the gauge. Always stand to the side of the gauge face the first time you open a tank.
- Reading flow with the torch valve closed. Static pressure does not reflect actual shielding gas flow. Pull the MIG trigger or open the TIG valve before setting flow.
- Skipping a leak check at the cylinder neck and hose fittings. A compatible leak solution is faster and safer than listening for hiss.
- Removing the sintered inlet filter. It traps debris that would otherwise damage the seat and cause pressure creep over time.
- Overtightening the regulator onto the cylinder valve. Snug by hand, then a quarter turn with a wrench is usually enough.
- Buying a regulator with a flow range that is too wide. A 10–60 CFH unit on a thin-sheet TIG torch means most of your usable range sits in the bottom inch of the tube.
Welding Gas Regulator Comparison
| Process fit |
Typical flow range |
Inlet |
Outlet style |
Best use case |
| Thin-sheet TIG |
0–30 or 0–40 CFH |
CGA580 |
1/4-inch barb |
Aluminum, stainless, delicate joints |
| General MIG and TIG |
10–60 CFH |
CGA580 |
Dual 9/16-inch and 5/8-inch threads |
Mixed shop work |
| Heavy MIG or production |
10–60+ CFH, dual-stage preferred |
CGA580 |
Dual outlets |
Long welds, large nozzles |
| Multi-gas (Ar, He, CO2) |
10–60 CFH |
CGA580 |
Dual outlets |
Shops that swap shielding gases |
Reading Reviews the Smart Way
User feedback is most useful when you filter for patterns rather than individual complaints. Look for repeated praise about stable needle behavior, leak-free fittings, and gauges that stay clear after months of use. A regulator that holds calibration after six months of weekly welding tells you more than a glowing first-week review.
Pay attention to comments about hose quality if the regulator includes one. A stiff or kink-prone hose makes accurate flow settings harder, even when the regulator body itself is solid. Note whether buyers mention your specific welder brand. Most CGA580 units are universal, but torch-end fittings can still vary by manufacturer.
Maintenance and Reliability Signals
Brass bodies remain the standard for inert gas regulators because they resist corrosion and handle thermal cycling well. Over time, diaphragms and seals can harden. If you notice outlet pressure creeping up with the torch off, the seat or diaphragm likely needs service or replacement rather than a full regulator swap.
A high average rating combined with strong monthly purchase velocity is usually a more reliable signal than either metric alone. A product that thousands of welders keep buying each month, while maintaining a high rating over a long review history, is almost always holding up in real shops.
Frequently Asked Questions
What does CGA580 mean on a welding regulator?
CGA580 is the standardized inlet fitting used on most argon, helium, and argon/CO2 shielding gas cylinders in North America. Confirm your cylinder valve matches before ordering.
Do I need a flowmeter or a dual-gauge regulator?
A flowmeter shows actual cubic feet per hour with a floating ball, which makes it easier to set precise flow rates. A dual-gauge regulator shows cylinder and outlet pressure, which is useful for diagnostics. Many welders prefer flowmeters for daily setup and use a dual-gauge model as a backup or for specific tasks.
Can one regulator handle both MIG and TIG?
Yes. A 10–60 CFH flowmeter with a CGA580 inlet typically covers both processes, although a 0–40 CFH unit gives finer control for thin-sheet TIG.
How long does a welding gas regulator last?
With normal shop use and occasional seal service, a quality brass regulator can last many years. Watch for pressure creep, fogging gauges, or inconsistent flow as signs that service or replacement is due.
Is a longer hose better?
Only if your shop layout benefits from the extra reach. An 8.2-foot hose lets you park the cylinder farther from the weld table, while a 6.6-foot hose keeps a compact cart tidy. Measure your workspace before choosing.
Do I need a dual-stage regulator?
Dual-stage regulators keep outlet pressure more stable as cylinder pressure drops, which helps during long welds or production work. For hobby and small-shop use, a single-stage flowmeter is usually sufficient.
Final Recommendation
If you want one regulator that handles the widest range of MIG and TIG tasks, choose a flowmeter model with a 10–60 CFH range and dual outlet sizes. It will cover thin-sheet TIG work through heavier MIG fabrication without forcing a second purchase. For welders who primarily run TIG on aluminum or thin steel, a 0–40 CFH regulator with precise ball-type metering offers better low-end control and more efficient shielding on delicate joints.
Budget-minded builders should look for a well-reviewed CGA580 regulator with a compact dual-gauge layout that delivers accurate pressure reduction without extras they will not use. For professional shops, a dual-stage regulator with strong warranty coverage stabilizes outlet pressure more effectively as the cylinder empties, reducing flow variation during long welds. Match the unit to your process, cylinder type, and shop layout, and you will spend less time troubleshooting gas flow and more time laying clean beads.